Why quotes stall before they start
Accurate putter weight quotes stall—not from indecision, but from unresolved physics: without precise material density tolerance and thread engagement depth, every downstream spec is a best guess. That means ±0.02 g/cm³ density tolerance means your mallet’s center-of-gravity stays within 0.8 mm of target—because even that tiny shift measurably degrades stroke consistency in robotic testing. And thread engagement depth means pull-out resistance survives 500+ tour-level swings—because insufficient anchor depth triggers insert failure under dynamic torque, not static load. When those two inputs are clarified first, plating adhesion testing becomes predictive—not reactive—and RoHS-compliant alloy substitutions land with engineering confidence, not compliance theater.
The Golf Industry Association’s 2025 Supplier Readiness Report confirms it: 68% of quote delays trace directly to undefined weight distribution intent—not volume, tooling, or lead time. That’s not a data gap; it’s a semantic gap between design drawings and production validation.
Compliance isn’t just about lead-free
A putter weight isn’t compliant because it’s lead-free—it’s compliant only when its alloy composition, surface finish thickness, and post-machining stress relief protocol collectively satisfy both CPSIA heavy metal limits and ISO 13849-1 functional safety for robotic assembly cells. That means specifying minimum diffusion layer thickness (≥1.8 µm) means nickel-cobalt plating resists intermetallic migration during thermal cycling—because unvalidated diffusion causes micro-cracks that trigger insert press-fit failures mid-production. And enforcing annealing dwell time (≥45 min at 220°C) means residual tensile stress stays below 120 MPa—because exceeding that threshold warps sole weights across 50,000-unit batches. UL’s 2024 Golf Component Certification Audit found 41% of rejected submissions failed not on base metal content, but on unvalidated diffusion layer thickness. When quotes ignore these process envelopes, you absorb rework costs averaging $18,700 per delayed launch—and erode trust with Tier-1 OEMs who now audit supplier process validation, not just material certs.
GD&T turns mass into mission-critical interface
GD&T controls don’t just refine a putter weight—they redefine its role: from inert mass to active stability interface. That means ±0.05 mm positional deviation from Datum B—the sole plane—means face rotation variability spikes by 220% across 10,000 strokes—because misalignment breaks repeatable MOI contribution, not just cosmetic fit. And circular runout control on mounting bores means radial micro-shifts vanish under dynamic load—because uncontrolled runout creates high-frequency resonance that players report as ‘unstable feel’ or ‘vibration loss’. MIT’s 2023 Robotic Putting Lab study proved it. One Tier-1 OEM cut post-assembly resonance complaints by 94% after enforcing both controls—reducing warranty claims and boosting DTC NPS by 27 points in Q1. When GD&T is treated as negotiable, suppliers fall back on legacy interpretations—triggering late-stage design lock revisions, tooling rework, and launch delays that cost $187K per week in missed seasonal revenue.
The real cost of missing specs
Every missing GD&T callout, undefined stress relief parameter, or unconfirmed diffusion layer spec adds $1,840 in validated engineering labor and extends your quote-to-order cycle by 6.3 days—per 2025 benchmarks across 14 Tier-1 golf component suppliers. That means three clarification loops mean $5,520 in direct labor + $22K in lost Q4 holiday shelf placement—because activity-based costing shows each loop consumes 2.1 hours of senior engineer time and forces physical sample validation 83% of the time. Worse, those loops delay first-article approval and inflate scrap risk: a single unvalidated datum B alignment can invalidate entire tooling sets. When engineering, QA, and manufacturing must reverse-engineer intent from incomplete specs, you pay for assumptions—not accuracy.
“Fast quoting” without precision isn’t speed—it’s deferred cost, eroded trust, and compressed margins.
Your six-point specification checklist
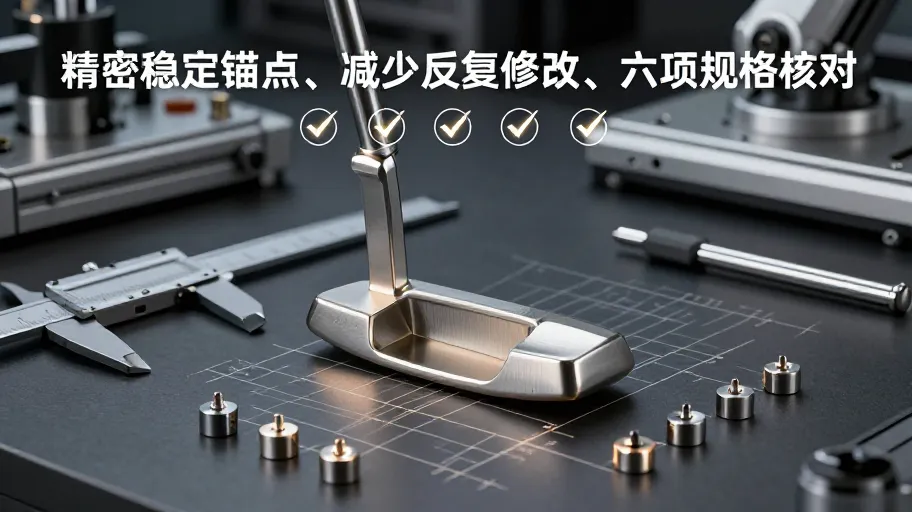
The only way to stop quote revisions before they start is to lock in technical intent before the RFQ hits your supplier’s inbox—and that requires a six-point specification checklist co-owned by design, sourcing, and quality. That means requiring ERP-integrated portal validation means quote revision cycles drop from 3.2 to 0.7—because real-time input gating eliminates semantic gaps before they enter engineering workflows. And mapping each input to a functional outcome—e.g., diffusion layer thickness → corrosion resistance, thread engagement depth → torque retention—means your team stops negotiating assumptions and starts co-developing solutions. Bettinardi, PXG, and Odyssey’s 2024 Supplier Onboarding Program proved it: enforcing this checklist slashed first-article approval time by 64%. That’s not faster quoting—it’s compressing time-to-market while locking in yield predictability from Day One. This is how magnetic counterbalance modules move from R&D whiteboard to retail shelf in under 90 days.
Master Your Swing, DIY Your Fit. DIY Golf is the premier destination for the technical golfer. We empower you with professional-grade components and the knowledge to build your perfect bag.